Showing posts with label Shop Projects. Show all posts

Thursday, May 6, 2021

Trash to Treasure -- How to Make Stuff from Scrap HDPE

 Overview

Five or six years ago I ran across an article where some guy had melted down some empty plastic milk jugs and used the material to make the head for a mallet.  While I'm not exactly an environmentalist, the cheapskate in me was attracted to the idea of making something useful out of apparent trash, so I decided to try it myself.  I've been fooling with the process off and on since, and figure it's time to add what I've learned to the existing folklore.

On the surface it's all pretty simple.  You melt a bunch of plastic scraps together, maybe transfer the resulting blob into a mold, and let it cool.  There's a pretty good series of three YouTube videos that starts here where a gentleman named Randy Knapp shows how he does it, with what I consider to be exceptional results.

Material Selection


The first thing to figure out is what kind of plastic to use.  From what I can tell, the best candidate for doing all this at home is High Density Polyethylene, or HDPE.  You'll find plenty of it in your trash can.  It melts at a reasonably low temperature, and it won't give off a bunch of toxic fumes when heated.  You can easily identify HDPE by looking for a triangular recycling symbol with the number 2 in it.

Unfortunately, not all HDPE is the same.  When heated, some variants form into a rubbery sticky blob that has to be more or less forced into a particular shape.  Others become almost liquid so that they will settle by gravity alone to completely fill whatever container they're in.  The measure of this "runniness when heated" quality is called the melt flow index, or MFI.  Wikipedia has lots more to say about it here.  If you poke around on Dow Chemical's website, you'll find a huge variation in the MFI (and other parameters, too) among their HDPE products.

This brings up the question: Do you want material with a high or low MFI?  The answer depends on how you plan to cast the material into the shape you want.  One way, as shown in Randy's video, is to let it cool in the same container you melted it in.  In this case, a high MFI is better because the HDPE will flow nicely into the container.  Any bubbles will (eventually) rise to the top, and with luck the result will be a solid block of uniform material.  Although Randy clamps a board over the top of the material after it has started to cool, I haven't seen where this has much benefit when cooling in the same container that was used for melting.

As mentioned, HDPE with a lower MFI doesn't really melt.  Instead, it sort of softens into a rubbery, sticky blob.  You can deal with it, however, by manually kneading it and twisting it while hot (You'll need gloves for sure!) to force out the bubbles, perhaps several times as more and more material is added to the mix.  Then when enough material is ready, you can let it solidify in a mold with a lid that allows you to apply clamping pressure to force the blob into the mold.

You'll notice (and be disappointed) that the HDPE items in your trash can don't have the MFI printed on them along with the recycling symbol.  So, short of heating it up and seeing how it behaves, how do you tell what you've got?  Here are a couple of hints based on what I've observed:

1.  The two common ways to make HDPE parts are blow molding and injection molding.  There's a good description of the differences between them here.  In general, the MFI of blow molded items like milk jugs, bottles, and similar hollow, thin-walled containers will be lower than that of injection molded items.  You can expect, then, that milk jugs and bottles will soften into the "sticky rubbery blob" state, and that material that was originally injection molded will tend to settle by gravity into the container it's melted in.

2.  Among different samples of injection molded material, those with the highest MFI will be the most flexible for a given thickness.  I say this based on my own observations, along with the statement from the Wikipedia article mentioned earlier that "The plastics engineer should choose a material with a melt index high enough that the molten polymer can be easily formed into the article intended, but low enough that the mechanical strength of the final article will be sufficient for its use."

One last hint on material selection is to try to use as close to the same material as you can in any given batch.  It's tempting to just throw together bits and pieces of whatever's lying around, but if you try to mix material with different characteristics, you're much more likely to have problems with voids, cracks, and places where two different kinds of plastic don't fuse together properly.

Melting

When it's time to melt a batch of HDPE, about all you have to do to get it ready is to make sure it's clean, then cut it up into pieces that will fit in your melting container.  If you have a bunch of really odd-shaped items, it might be useful to shred them so they pack efficiently into your container.  But otherwise I don't think shredding has any benefit.

You'll want to melt your plastic in an oven at about 350 degrees F.  HDPE has very poor thermal conductivity, so if you're dealing with thick blocks of material, it will take a long time for them to heat throughout.  Avoid the temptation to speed the process by raising the oven temperature.  If the oven gets too hot, the plastic will burn and smoke and you'll get an icky brown layer on the surface of the material.

If you're using plastic with a high melt flow index, it will be easy to see when the material has become semi-liquid and started to flow into the pan.  But it's not so easy to tell when the bigger pieces have melted completely.  It's also not easy to tell when all the bubbles have risen to the top and popped.  For both of these reasons, it a good idea to let the batch cook for a good long while before you let it cool and solidify.

Mold Options


As shown in Randy's video, a non-stick brownie pan works well if you plan to cool the material in the same container you melt it in.  The non-stick surface and the sloped sides make it easy to remove the cooled plastic from the pan.

However if you want to use low-MFI material, you will need a mold that somehow allows you to clamp down on a lid to force the plastic into the mold under pressure.

I prefer the high-MFI, cool-in-the-melting-pan approach myself, but sometimes don't want to make a whole brownie pan full.  So I sort of went overboard and made this mold where you can move one side to make blocks of various sizes:

This thing just barely fits in my thrift shop toaster oven.  It doesn't have a non-stick coating or any draft to aid in removing the cast plastic, but since it comes apart, this isn't a problem.  Naturally, you have to plug up the unused holes to prevent the plastic from leaking out.  When I do find myself needing to compress some low-MFI material under pressure, I just cut a piece of plywood to match the current position of the moveable partition, and squish it down with C-clamps.

Working the Plastic


Once you have a nice block of HDPE, you'll be happy to discover that you can work it with most any of your woodworking or metalworking tools.  In particular, it's a lot of fun to machine on a mill or a metal lathe because you can remove material much faster than you would ever dream of with metal.

About the only thing that doesn't work is sandpaper.  HDPE is pretty resistant to abrasion, and when you try to sand it--especially by hand--nothing much happens.

My Projects


Here are some of the things I've made from recycled HDPE.

I made this extremely crude oscillating cylinder engine a few years back as an exercise to see what I could do with the material.  HDPE tends to be slippery (sort of like Teflon), so it worked well for the engine's simple bearings, piston action, and the seal between the wobbling cylinder and the stationary upright.  Unfortunately, over time the plastic parts warped enough that the ending bound up too tight to run.  (More on that under "Limitations" below.)


These trunnions for the tilting table on a disk sander are another place where HDPE's slipperiness made it easy to get a tight, low-friction fit between two parts.


HTPE is waterproof, so it worked well for these replacement axles, bushings, and wheels for a pool sweeper.


This replacement walker ski takes advantage of HDPE's abrasion resistance.  It and its mate have been in use for a couple of years and show almost no sign of wear.

Limitations

Obviously, you'll be limited in how big a piece of HDPE you can cast by the size of your oven.  What's less obvious is that it's difficult to make very thick pieces.  In my experiments, blocks more than about 1-1/2" thick almost always have internal voids in them.  These flaws are not round like bubbles would be, but appear more like tears.

This is pure speculation on my part, but here's what I think causes these voids.  HDPE shrinks a lot when it cools.  (That's a fact.) Before it has a chance to solidify, this shrinkage is relatively uniform throughout, and the block just gets smaller.  But since the block naturally cools from the outside in, eventually the top, sides, and bottom solidify to make a rigid shell that surrounds the still-molten material inside.  Then as that material tries to shrink within the rigid shell, something has to give and the inner material basically tears itself apart.

Even if these internal voids don't materialize, I believe that the cooling process creates internal stresses in the material.  These are what probably caused the warping over time of the parts in my little wobbler engine.  As it turns out, you can anneal the material to help mitigate this problem.  This website [] has more details on that process.

One last problem is that most adhesives won't stick to it at all. I've never had any luck trying to weld it, either. But bolts and nuts and screws all work, so it is possible to fabricate items with multiple parts if you don't mind using mechanical fasteners.

Saturday, January 20, 2018

Drill Press Table Counterweight

My drill press features the "lift it up and down with your hand" method for adjusting the table height.  This got old after a while, especially with a vise or a heavy workpiece on the table, so I started looking for a way to add a counterweight to make the process easier.

The best setup I found on the internet had a cable running up from the back of the table, over a pulley at the top of the column and then down inside the column to the counterweight itself.  Unfortunately, I couldn't make this work on my drill press because the motor mount was in the way of the cable.  There was also no really good way to attach a cable to the back of the table.

I eventually figured the next best thing would be to have pulleys just below the drill press head with the counterweight riding outside of the column.  The pictures show how I did it.

The bracket that holds the pulleys is made of red oak, and clamps to the drill press column with some long bolts.  The axles for the pulleys are 1/4-20 bolts that I just screwed into threaded holes tapped into the oak.

I machined the pulleys themselves from high density polyethylene (HDPE) scraps that I melted in an oven and then cast into a block under pressure in a wooden mold.  (That's another story altogether--this YouTube video and the very first part of this one show how to do it.) The HDPE plastic is kind of slippery, so I didn't need any fancy bearings or anything to make the pulleys work for this project.

The counterweights are simple wooden boxes with sand in them.  I adjusted the amount of sand in the boxes until the weight seemed about right.  In the end I think the whole assembly wound up about three pounds lighter than the table.

Sunday, March 1, 2015

Small Parts Storage Trays


Here’s yet another way to store nuts and bolts and screws and whatnot. These trays are made from scraps of 1/4” MDF and 1/8” tempered hardboard left over from other projects.


I sized them so they will sit up on edge in a couple of the drawers in my work bench. That makes it easy to remove any one by itself while still utilizing most of the space within each drawer. For that to work, though, the sliding lids have to fit nicely against the dividers so the hardware doesn’t get all mixed up when the tray isn’t sitting flat.


You could also store them like books on a shelf.


To keep track of which tray contains what, I made an Excel spreadsheet on my computer that lists the contents of each tray. I keep a printed copy in the drawer with the trays so I can find the correct tray pretty quickly when I want to deposit or withdraw some random bit of treasure.

Monday, February 23, 2015

Biesmeyer-Style Bandsaw Fence - Free Plan

I have a Taiwanese clone of the Delta 14" bandsaw that I bought used without a fence.  That didn't bother me too much at first, because I thought that I would be using it to cut curves most of the time, and that when I did need a fence, I could just clamp a board to the table.  But then I found out how useful a bandsaw is as a ripping machine and for certain kinds of joinery, and how tedious it is to accommodate drift using the clamp-a-board-to-the-table method.

I needed a real fence.

I thought about building the shop made fence described by Patrick Sullivan in Fine Woodworking #210.  But when I looked at it closely, the design seemed overly complicated to me.  So I set out to build something simpler that would still get the job done.  After a couple of false starts, I eventually came up with the Biesemeyer-style fence described here.

I started with a piece of 1-1/4" x 1-1/4" x 1/8" 6063-T5 aluminum channel for the rail.  I cut one leg off at 13/16" as shown in this drawing.  I then drilled it to match the mounting holes on my bandsaw table and cut a little notch to match the bandsaw's miter slot.

Then I made the "slider" shown in this drawing.  It rides to the left and right along the rail and clamps in place with a little bolt.  The longish piece on the bottom of the slider registers against the rail to align the slider, while the shorter piece carries a T-nut for the bolt that clamps the slider to the rail.  You could use a threaded insert instead of the T-nut if you want.  If you look carefully, you'll see a little piece of bent sheet metal that prevents the slider from marring the aluminum rail when you crank down on the bolt.  I called this thing the "rail protector", and it's shown in this drawing.


There are also two T-nuts in the holes on top of the slider.  These receive a couple of bolts that hold the base of the fence to the slider.


This drawing shows the base of the fence itself.  It's cut out on the left side to clear the bandsaw's yoke when the fence is positioned towards the left side of the bandsaw table.  The hole and the curved slot nearest the operator accommodate bolts that attach the base to the slider.  The curved slot allows the base to rotate in order to adjust for drift.

The other holes in the base have threaded inserts or T-nuts that allow attachment of the auxiliary high fence shown in this drawing.  It can be installed in either of two orientations for resawing or to accommodate various workpiece thicknesses.


You might want to use star knobs instead of the bolts that I have shown for the clamp bolt in the slider and the bolts that attach the base to the slider.  You might also might want to make the slider and base out of aluminum instead of wood!


Sunday, May 26, 2013

Super Simple Horizontal Boring Jig

I needed to drill some fairly accurate holes in the ends of a long board.  So I made this jig to hold my drill in a horizontal position.  I was careful to make the centerline of the drill parallel to the edge of the base.  That way I can line up both the jig and the workpiece with the long edge of my workbench to more or less guarantee a straight hole.


Saturday, November 12, 2011

Yet Another Box Joint Jig - Free Plan

Like most everyone in the world, I've posted a few of my projects on LumberJocks.com. So far, the most popular one has been this box joint jig. The basic idea came from Matthias Wandel's original box joint jig, but instead of a crank like Matthias used, I put a knob with a dial on mine to move the workpiece back and forth. I thought this was a little bit simpler and a little more versatile than Matthias's version with the crank.

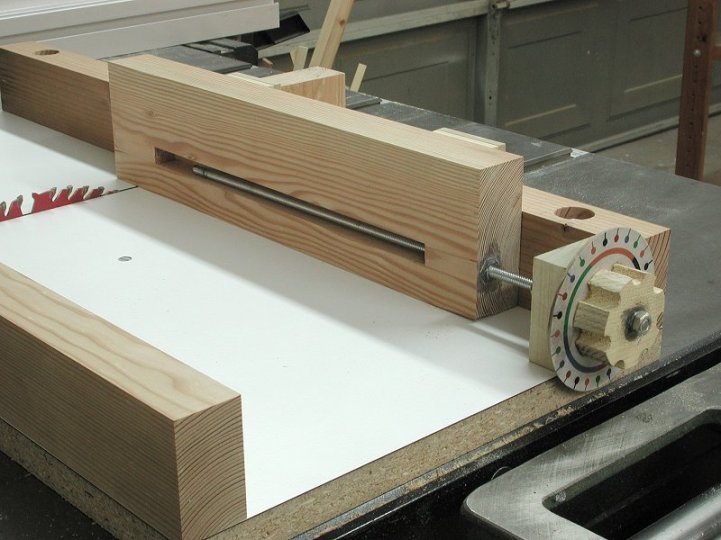
The jig is built by adding a sliding carriage to the rear fence of a standard crosscut sled. To use it, you clamp the your workpiece to the sliding carriage, and then turn the knob to precisely position the carriage for each successive cut. Each mark on the dial represents 0.002" of movement, so with a little planning, you can make any sort of box joint you want. More on that later.

The Details

If you want to build one of these yourself, the following pictures link to drawings that give the dimensions of the jig as I built it.  The table on my saw is about 27" wide, and the blade is about 16" from the left side of the table.  If your saw is substantially different, you may need to adjust the dimensions of the jig to suit your saw.  In particular, you must make absolutely sure that your saw cannot cut into the jig's metal lead screw.

Rear Fence
Bearing Block
Carriage
Lead Screw
Dial

Building the Jig

To build the jig, start by making a standard crosscut sled for your table saw.  Make the rear fence 2-1/4" tall and 1-1/2" thick, as shown in the first drawing above.  Make sure the rear fence is square to the saw blade.  This video shows a quick and straightforward way to square the fence on a crosscut sled.

Next, find a bearing to support the end of the lead screw near the dial.  Ideally, the bearing should have an inner diameter of 1/4" to match the 1/4-20 threaded rod used for the lead screw.  If you happen to have a bearing with a larger inner diameter, you can make it work with a bushing as shown in the photo nearby.  My bearing happened to have an outer diameter of 1-3/8".  Anything smaller than 1-1/2" or so would work.

When you have found a suitable bearing, make the bearing block shown in the second drawing above, except that the hole should fit your bearing.  Center the hole in the bearing block, and size it so that your bearing fits tightly into the hole.  Attach the completed bearing block to the left end of the crosscut sled's rear fence, as shown in the first two photos above.

Now make the carriage as shown in the third drawing above.  Use extra care when making the little hooks that ride over the fence.  You want the carriage to slide freely on the fence, but with as little play as possible.  There's nothing special about the big mortise that houses the lead screw;  it was just easier for me to make it that way than to try to drill a long hole lengthwise through the carriage.  (I guess there's also some comfort in being able to see the lead screw, in order to make double dang sure that you're not going to cut into it with the saw blade.)  Embed a 1/4-20 nut in the end of the carriage as shown in the drawing and in the first photo above.

Important:  When you have the carriage complete, add a block of wood to the backside of the rear fence as shown in the second photo above.  The purpose of this block is to protect your fingers from the saw blade at the end of each cut.  The block must fully enclose the blade as it comes through the back of the fence.  You will need to notch the top corner of the block as shown to allow the carriage to slide freely back and forth.  Do not use the jig without this block in place.

To make the dial, click on the image above to open a .PDF file that contains a full sized image of the dial.  When you print the image, the diameter of the dial should be 3-1/2".  Paste the printed image onto a piece of 1/8" plywood (or something similar), cut out the circle, and drill a 1/4" hole in the center.  Next make a knob of some sort, and cut the lead screw to length from 1/4-20 threaded rod stock.  Attach the knob and the dial securely to one end of the lead screw.  The knob and the dial must not be allowed to rotate on the lead screw.

Next, thread the free end of the lead screw through the bearing and install a washer and a pair of jam nuts as shown in the photo nearby.  When you're using the jig, you'll need to apply slight pressure to the carriage to ensure that the jam nuts ride tight against the bearing.  If you want, you could add some sort of spring arrangement to take care of this automatically.

Finally, position the carriage over the rear fence and thread the lead screw into its embedded nut by turning the dial.  Check one last time that your saw can't cut into the lead screw, and you're ready to go.

Measuring Your Kerf Width

With the jig complete, you can now make precisely spaced crosscuts by clamping your workpiece to the carriage and then turning the dial to move the workpiece after each cut. Before you can do much of anything useful, though, you need to know the width of the kerf that's taken by your particular saw blade. If you have a dial caliper or one of those fancy electronic ones, this is fairly easy to measure, as follows:
  1. Use your saw to rip a piece of scrap two or three inches wide. Make sure the edges are both straight and parallel to one another, then use the caliper to take a precise measurement of the width of the scrap.
  2. Rip the scrap down the middle into two pieces.
  3. Reassemble the two pieces next to each other, and measure their combined width.
  4. Subtract the combined width of the two pieces from the width of the original piece. This difference is the width of the kerf that was taken by your saw blade.
If you don't have a caliper, you will have to take as good a guess as you can, then make some trial and error adjustments later when you actually go to use the jig.

Cutting a Simple Box Joint

Probably the simplest box joint to cut is one where the fingers are the same width as the saw kerf.  That would be roughly 1/8" for a normal blade, or whatever you want if you are using a dado stack.  In any case, the joint involves a series of cuts that are evenly spaced by twice the width of the saw kerf.  So let's suppose that your kerf is 0.132" wide.  That means you want to move the carriage by twice that amount, or 0.264", after each cut.  So how do you do that?

If you're a math whiz (or maybe a machinist), you might realize that each dot on the dial represents 0.002" of carriage movement, and that the numbers on the dial represent thousanths of an inch.  From that, you could figure out how far to turn the dial based on the numbers, but doing so would involve some error-prone arithmetic for every single cut.  Fortunately, there's an easier way that's based on the pattern of colored arcs and dots on the dial.

Here's all you have to remember:
  • Rotating the dial by one dot's worth moves the carriage 0.002".
  • Rotating the dial by one arc's worth moves the carriage 0.010"
  • Rotating the dial one full turn moves the carriage 0.050"
So, in our example, to move the carriage by 0.264", you would turn the dial five turns to move it by 0.250", then one arc to bring it to 0.260", then two dots to reach 0.264".  So "five turns, one arc, and two dots" is all you have to remember (or write down), and it's the same for every cut.  This is actually a lot easier to do than it is to explain.  Once you've played with it a while, you'll do it without thinking.

Cutting More Complicated Joints

With the jig, you're not limited to any particular finger width or spacing, although more complicated joints do involve a little bit of planning.  But the fundamental process is straightforward:  Figure out how you need to space your cuts, turn the dial to put the workpiece exactly (!) where you want it, and have at it.

Saturday, April 23, 2011

How to Flatten a Cutting Board

December 22, 2006. That's the day when Marc Spagnuolo published A Cut Above, the Wood Whisperer podcast episode that transformed the end-grain cutting board from a utilitarian kitchen accessory to a near rite of passage among fledgling woodworkers everywhere.


In the video, Marc shows how to keep the boards aligned during the glue-up to minimize the need for sanding later. But if your pieces aren't cut exactly right, or if one of them slips without being noticed during the final glue-up, it's entirely possible to end up with a cutting board that's needs to be flattened before you can finish it.

Your first thought at this point might be, "I'll just run the board through my planer." That sounds like a reasonable idea, but DON'T DO IT! Planers don't like to plane end grain. Even with extreme care, there's a really good chance that you'll destroy the board, and maybe the planer as well.

So what to do? If you have a thickness sander (or access to one), that's the way to go. If you don't, you might have success with a hand-held belt sander or with hand planes. However, it takes some finesse to get a board flat with a belt sander, and it's not especially easy to use a hand plane on end grain.

In the absence of a thickness sander, another option is to use a router and a jig. This setup is really neat, even though it would certainly be overkill for a little cutting board. This one is similar, but scaled down a bit for smaller boards. Both of these jigs (and many others) rely on some sort of straight rail system to guide the router.

It occurred to me that a flattening jig might use the surface of a workbench or assembly table as a reference, instead of having rails built into the jig. With that idea in mind, I came up with this very simple jig:


It acts as a bridge, suspending the router a fixed distance above the workbench. To use it, I secured the workpiece to the workbench, and then just slid the jig around on the workbench to flatten the board. I didn't have a cutting board to try it out on, so I used a big block of fir that I had laying around instead.

I got some burn marks that started after the cheap HSS router bit I was using got dull when I went through a big knot. I don't think you would get this burning with a decent, sharp carbide bit in clear lumber.

For this experiment, I just clamped the legs on either end of the jig to raise it above my big thick block. For most applications, where the workpiece would typically be an inch or two thick, you could attach the legs permanently and then tweak the router itself for small vertical adjustments.

I mounted the router a third of the way from one end of the jig. With this arrangement, if you plane the right half of the board with the router oriented towards the right, then turn the jig around the other way to do the left half, you can plane boards that are 2/3 as wide as the jig is long. If you mount the router in the middle of the jig, there's no need to turn the jig around, but you'll be more limited in the width of boards that you can flatten.

Tuesday, April 12, 2011

Bandsaw Outfeed Table

When I first got a bandsaw, I thought I would use it mostly for cutting curves, and maybe once in a while for sawing small logs into boards. But pretty soon I figured out that it was every bit as useful as a ripping machine, especially with warped or twisted stock that would be just plain dangerous to cut on a table saw. So of course that meant I needed something to support longer boards as they came off the back of the bandsaw.

This is what I came up with. One end attaches firmly to the bandsaw table, while the other end sits on a single leg that's hinged so it will fold up for storage. A piece of clothesline rope keeps the leg from swinging out too far when the table is in use. I'm the first to admit that this arrangement looks pretty flimsy, but it is surprisingly stable when it's all set up.

To attach the outfeed table to the bandsaw, I started by bolting a piece of aluminum angle to the bandsaw table. The holes for the bolts were already drilled and tapped in the bandsaw table. The outfeed table then sits on the little shelf formed by the aluminum angle. It is held in place by two more bolts that go down from the top and through the angle.

When I made the outfeed table, I had to include a shim to bring its top surface up to the level of the bandsaw table. I also had to cut a couple of notches in the end of the outfeed table to clear the heads of the bolts that attach the angle to the bandsaw.

The length of the leg is adjustable to make it easy to level the outfeed table, regardless of how the floor slopes or doesn't slope. At one time I also used the outfeed table with a radial arm saw, and the adjustable leg accommodated the difference in height between the bandsaw table and that of the radial arm saw.

I have no idea what I was thinking when I made this hinge to attach the leg to the table. A metal one from the BORG would have been much, much simpler.

Sunday, March 20, 2011

Shop Cart with Adjustable Shelves - Free Plan

This fabulous item is a roll around computer cart with adjustable shelves.  At least that's what I thought it was about thirty years ago when I made it and three or four more identical clones.  The idea was to put the monitor and a keyboard on the top shelf, with a printer and the computer itself on the two shelves below. There was no room for a mouse, but that was not a problem because computer mice didn't really catch on until about 1984 when the Apple Macintosh first came out.  Unfortunately, there was also no room for your knees, either.  Duh.  That really was a problem, given that knees had achieved widespread popularity quite some time earlier.

The good news is that these carts were useful anyway.  I wound up using a couple of them for many years to store books, and gave a couple of them away to friends for who knows what.  And I still have one in my shop.  It's handy enough for all sorts of things that I would build another one tomorrow if I was starting over from square one.

The Details

If you want to make one of these yourself, the following pictures link to PDF files containing dimensioned drawings of all the parts.

Side

Base

Shelf

I made the base from a piece of 1/2" plywood, with a 3/4" thick solid skirt to trim up the edges of the plywood and provide a way to attach the sides.  Although the drawing shows it being put together with simple butt joints, you would probably want to use some screws or fancier joinery to make it a little more robust.  There are four pads glued to the underside of the base for mounting some casters.  The exact size and thickness of the pads will depend on the specific casters that you are using.

The shelves are similar to the base, except that the skirt is narrower and they have holes drilled for two T-nuts in each side. Bolts go through the sides of the cart and into these T-nuts to support the shelves. Because the base and the shelves all need to be the same size, it's a good idea to make them all at the same time. I made three shelves (in addition to the base) for each cart, but I don't think I ever used more than two at a time.

The sides are made from 3/4" stock. I used half lap joints at the corners. Mortise and tenon joints would work instead, as would floating tenons or even pocket screws. I drilled 5/16" holes for the 1/4" shelf mounting bolts so it would be easy to get everything lined up when installing the shelves. The sides are glued permanently to the base, and have a 1/4" roundover on all the outside corners just for looks.

The ugly drips of paint are completely optional.

Monday, February 21, 2011

Bandsaw Dovetail Jig - Free Plan

Something got into me a couple of weeks ago and I decided for no particular reason to try to make some hand-cut dovetail joints. The results were not good at all, partly because I don't have a proper dovetail saw, but mostly because my saw kerfs were not even in the same county as my cut lines.

So rather than upgrading my saw and simply repeating the failure with a different tool, I decided to try a method I had read about in separate articles by Lonnie Bird and David Marks. These guys both cut their pins first on the bandsaw, using a system of spacers along with the bandsaw's fence to guide the cuts and to establish the layout of the joint. After chiseling out the waste between the pins by hand, they then mark the tails and cut them freehand on the bandsaw. Finally, they chisel the waste from between the tails to complete the joint.

Besides the spacers, Bird and Marks both describe a sloping auxiliary table that you need if your bandsaw doesn't tilt to the left.

This technique appeals to me for a number of reasons:
  1. You can cut dovetails even if you can't saw to a line. Yay!
  2. You don't need any fancy and expensive equipment.
  3. You can size and locate your pins any way you want.
  4. It eliminates most of the tedious measuring and layout required for hand-cut joints.
The one thing I don't like is the spacer idea. Making the spacers seems simple enough, but figuring out how wide they should be looks to be fairly confusing. In The Bandsaw Book, Lonnie Bird tells how to make the spacers for evenly spaced pins, but doesn't explain what to do if you want variable pin spacing. Most of the other descriptions I've seen either ignore the problem, or else cop out completely with nonsense like, "some experimentation will be needed to determine the width of the spacers." Great.

Rather than messing with the spacers, to me it seems simpler to just mark the desired pin positions, then saw them using the fence to help keep the cuts straight and square to the end of the board. If you're making multiple joints, you still only have to mark one part, set the fence, and then use that one setting for all the corresponding cuts on the other boards.

The Jig

My bandsaw doesn't tilt very far to the left, so I needed to build the sloping auxiliary table. As I was thinking about how to make it, I realized that it would be easier to use if the fence was part of the auxiliary table than it would be to adjust the bandsaw's fence and move the auxiliary table for every cut. With that in mind, here's what my jig looks like:


The small cleat on the right side squares the jig with respect to the bandsaw table, while the C clamp just keeps it from moving around. The slope of the platform determines the slope of the pins and tails.  The fence assembly slides in a dovetailed (!) slot in the platform, and is held in place with a second clamp once set.

The following images link to PDF files containing detailed drawings of the jig as I made it.  It's sized to fit my generic 14" bandsaw. There's nothing especially critical about any of the dimensions, however, so the plans should be easy to modify for use with other bandsaws. I used 5/8" particle board and 1/4" tempered hardboard for my jig. There's nothing critical about that, either.

Base
Platform
Fence

How to Use It

Cutting dovetails using this jig is much like cutting them by hand using the pins-first method, except 1) you use the bandsaw instead of a hand saw to cut the pins and tails, 2) the layout of the joint is much simpler, and 3) if you're doing multiple joints, you only have to do the layout once.  Given that similarity, there's no point in rehashing all the gory details of hand cutting dovetails when they've already been expertly discussed many times before.  Instead, I'll just give a quick (?) step-by-step run through, with some pictures to show how the jig works.

In case you're new to the subject, there are a couple of entries (Part 1 / Part 2) in Glen Huey's blog that explain the pins-first method in great detail.  There's also a very nice video in Keri Hultman's blog that's definitely worth a look, if only to see how she uses a big fat plane blade to position a block to guide her chisel.

Stock Preparation and Layout

After you've milled your stock to be flat and square in every direction, use a marking gauge to mark baselines on both the pin board and the tail board, just as if you were going to cut the joint by hand.

Then lay out the locations of the pins. I like to do this with a knife just for the sake of precision. I also like to make rough pencil marks on the end of the board to indicate the ends of the pins. These don't have to be accurate; they're there simply to reduce confusion when actually cutting the pins. The layout shown has a half pin on each side of the board, with two full pins spaced relatively close to the half pins. This will result in two small tails next to the half pins, and a single, wider tail in the middle.

Cutting the Pins

To cut the pins, set up the jig as shown, with the small cleat on the right side and the platform sloping up and to the left. Register the cleat against the edge of the bandsaw table so the jig is square, then secure the jig with a small C clamp.

Now hold the workpiece against the fence on the jig, and move the fence so that the bandsaw blade is lined up on the waste side of the mark that defines the half pin farthest from the fence. (This will be the right side of the leftmost half pin as viewed from the normal operator's position.) Apply a small clamp to keep the fence from moving. Verify the setup by comparing the blade position with the rough pencil marks on the end of the board. If everything looks good, use the jig's fence as a guide to make the cut from the end of the board to as close to the baseline as you dare. If you are making multiple joints, leave the fence set and make all the corresponding cuts on the other pin boards.

Now move the fence so the blade is lined up with the right-hand side of the next pin. As before, clamp the fence in position and check the blade position against the pencil lines on the end of the board. When everything is ready, make the cut. Repeat this process until you have a cut on the right-hand side of all the pins on all of your pin boards.

To finish cutting the pins, turn the jig around 180 degrees so the cleat is registered against the left side of the table, and secure it with a clamp. Now the board will be angled the other way and you can make the cuts on the left sides of all the pins.


With all the pins defined, you can use the bandsaw to remove much of the waste between the pins. Do this by making repeated freehand cuts in the spaces between the pins. Stop these cuts 1/16" or so from the baseline, and make sure that you do not cut into any of the pins. Finally, break out the thin slivers left by the bandsaw, then chop the remainder of the waste from between the pins using a chisel in the traditional way.

Cutting the Tails

Mark the tails from the pins just as you would if you were cutting the joint by hand. Again, I like to use a knife for greater precision, followed by a tap with a chisel if needed to make the marks deeper and easier to see.

With the jig removed from the bandsaw, carefully saw out the tails freehand. Make sure to keep the blade on the waste side of the cut line, and don't cut past the baseline. As you did with the pins, make repeated freehand cuts between the tails to remove most of the waste in preparation for chopping.

Finally, chop the remaining waste from between the tails using a chisel. Adjust the fit, assemble the joint, and throw it on the heap with all of your previous attempts.